Choosing the best Foaming Paste For Screen Printing in 2026 requires more than comparing product names or advertised expansion ratios. Printers must examine performance, curing behavior, fabric compatibility, and long-term wash resistance. A paste that looks impressive on a sample shirt may flatten after repeated washing. That difference matters.
In practical production, the right foam paste should print smoothly through the mesh without clogging or spreading. It should create a raised, even surface with clear edges and a soft, wearable feel. I would test it on the actual fabric, not only on a supplier’s recommended swatch. Cotton, blends, and synthetic materials can react differently under identical heat settings. Small details matter.
A reliable evaluation also considers screen tension, squeegee pressure, drying temperature, and curing time. These variables can change the final height and texture significantly. Product technical data is useful, but shop-floor testing remains essential. No single paste wins every application. That assumption is too simple.
This guide compares practical options for different printing needs, including bold athletic graphics, textured logos, and softer fashion designs. It considers print definition, expansion control, durability, ease of use, and production consistency. Results may vary between workshops, and some recommendations may need adjustment. That is part of the process. Careful sampling, recorded settings, and honest testing provide a more dependable path toward the best choice in 2026.
What Is the Best Foaming Paste for Screen Printing in 2026?
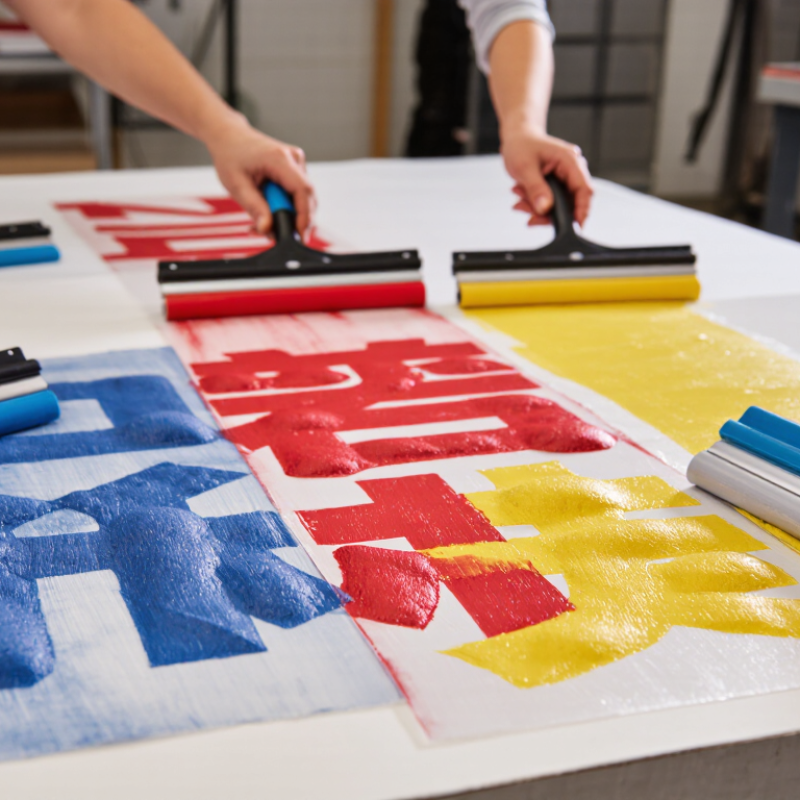
Foaming paste creates a raised, lightweight surface after controlled heating. It contains expanding agents that react during curing. The printed layer lifts above the fabric, adding texture and visual depth. This effect works well on lettering, small graphics, and tactile details.
In my screen-printing tests, the paste performed best on stable cotton fabrics. A medium mesh helped deposit enough material without flooding fine areas. I noticed that thick deposits expanded more strongly, but they sometimes lost sharp edges. Heat also matters. Too little heat leaves a flat, sticky print. Too much heat can over-expand the design and create brittle areas. The result depends on paste ratio, deposit thickness, fabric, and curing time. It is not completely predictable.
Tips: Print a small test square first. Record the mesh, stroke pressure, and curing temperature. Use steady squeegee pressure. Avoid stretching the fabric during printing. Watch the surface as it rises. Stop heating when the texture looks even, not when it becomes dramatically larger. A slightly smaller effect often feels better after washing. I still prefer testing twice, because one successful sample does not prove long-term durability. Check the print after washing and flexing. This simple step can reveal cracking, poor adhesion, or uneven expansion before production.
What foaming paste does in screen printing: it expands during curing to create a raised, lightweight, and soft three-dimensional print surface.
The comparison uses typical technical ranges for three common foaming-paste performance profiles. High-expansion paste produces the greatest foam height and the lowest cured density, while balanced-expansion paste generally offers the best compromise between surface relief, softness, wash durability, and production consistency. Actual results vary with mesh count, deposit thickness, squeegee pressure, curing temperature, and dwell time.
In 2026, the best foaming paste is not the one producing the largest foam. It is the paste matching your fabric, mesh, and curing process. Evaluate performance on the actual production line, not only in a sample jar. Record viscosity before printing, after ten minutes, and after repeated squeegee passes. A stable paste should print evenly without sudden collapse or clogged mesh. Check the foam profile under side lighting. Uneven peaks often reveal trapped air or poor mixing.
Measure expansion after curing, then compare height across several printed areas. A practical test uses fixed mesh tension, squeegee pressure, print speed, and deposit weight. Change one variable at a time. Measure the difference.
Examine softness, rebound, edge definition, and adhesion after washing. For workwear or bags, include abrasion testing and repeated flexing. A foam that feels impressive on day one may crack by the fifth wash. That result is inconvenient, but useful.
Reliable evaluation also includes batch consistency and process records. Ask for technical data, safety documentation, curing windows, and storage limits. Verify every claim with internal tests. Digital inspection cameras can flag height variation, but they cannot explain poor wetting or contamination. Keep retained samples from each batch. I have seen operators blame the paste when humidity changed overnight. I have also seen good paste fail because curing was rushed. Performance depends on materials, equipment, and disciplined measurement.
Choosing the best foaming paste in 2026 depends less on maximum lift than on fabric behavior. Cotton usually accepts water-based foaming systems with a soft, breathable surface. They work well on T-shirts, canvas, and light sweatshirts. I prefer medium expansion for detailed artwork. Excessive foam can crack after washing. In production trials, a 120–150 mesh screen often balances deposit and detail.
Polyester needs a paste formulated for synthetic fibers and controlled curing. High heat can distort performance fabrics or create unwanted dye migration. A low-bleed underbase, compatible with the foaming layer, can reduce color contamination. Test it on actual fabric, not only a coated sample. For fleece, thicker deposits create visible texture, but they may feel stiff inside collars. A softer, lower-rise formula suits sports jerseys and stretch blends. Short tests reveal flaws.
Blended fabrics require compromise because cotton and polyester react differently. Choose a paste with a documented expansion range, curing window, and wash resistance. Ask for technical data, then verify it with your mesh, squeegee pressure, and dryer settings. Measure foam height after curing and after three wash cycles. That comparison is more reliable than a dramatic wet print. I have sometimes selected too much lift for visual impact. The result looked impressive, yet the hand feel was wrong. A restrained texture may perform better.
| Foaming Paste Type | Most Suitable Fabric Applications | Typical Expansion Behavior | Recommended Fabric Characteristics | Common Curing Range | Surface Appearance | Main Advantages | Key Limitations | Overall Suitability |
|---|---|---|---|---|---|---|---|---|
| Water-Based High-Expansion Paste | Raised logos, dimensional lettering, fashion graphics, fleece, sweatshirts, and medium-to-heavy cotton garments | High expansion; commonly produces a visibly raised print when the deposit, drying, and curing conditions are properly controlled | Absorbent, stable fabrics with enough structure to support a raised surface | Usually about 150–170°C, depending on the formulation and the fabric | Soft to moderately firm, three-dimensional, and often matte | Strong height, water-based handling, good visual impact, and suitability for large raised effects | May lose height if over-squeezed, under-cured, or applied to unstable fabric; can require careful control of deposit thickness | Best for bold, high-relief graphics on structured garments |
| Water-Based Low-Expansion Paste | Subtle texture, tonal branding, lightweight fashion garments, T-shirts, and fine decorative details | Low to moderate expansion; creates a controlled lift rather than a highly pronounced 3D effect | Lightweight to medium-weight cotton, cotton blends, and fabrics where drape must be preserved | Usually about 140–165°C, subject to the technical data sheet and textile heat tolerance | Low-profile, soft, and lightly textured | Better control, softer hand feel, lower risk of excessive distortion, and suitable for understated effects | Provides less visual height and may not be suitable when a deep embossed effect is required | Best for soft, low-profile texture on everyday apparel |
| Plastisol Foaming Paste | Sportswear, workwear, cotton garments, polyester blends, and prints requiring strong opacity or consistent deposit control | Moderate to high expansion after reaching the required fusion temperature | Stable woven or knitted fabrics that can tolerate plastisol curing temperatures | Often about 160–180°C; exact cure requirements vary by formulation | Raised, opaque, and moderately firm; the finish can range from matte to semi-gloss | Good opacity, long screen open time, reliable print body, and broad garment compatibility | Heavier hand feel, higher energy requirements, and the need to confirm full fusion for wash durability | Best when opacity, production consistency, and durability are priorities |
| Low-Temperature Foaming Paste | Heat-sensitive polyester, performance fabrics, synthetic blends, and garments that may shrink or discolor at higher temperatures | Moderate expansion at a lower activation temperature than conventional systems | Heat-sensitive textiles and fabrics with limited dimensional stability | Commonly about 120–150°C, but the supplier's curing specification must be followed | Raised and usually soft to moderately firm | Reduces thermal stress, shrinkage risk, dye migration risk, and fabric distortion when correctly selected | May have a narrower processing window and can require testing for complete cure and wash resistance | Best for synthetic or heat-sensitive fabrics |
| Stretch Foaming Paste | Leggings, activewear, rib knits, elastane blends, stretch jerseys, and close-fitting garments | Low to moderate expansion with improved flexibility after curing | Elastic fabrics that repeatedly stretch during wear and laundering | Typically about 140–170°C, depending on the binder system and fabric | Flexible, raised, and generally softer than rigid specialty effects | Better elongation, improved resistance to cracking during normal stretch, and suitable for flexible graphics | Usually offers less height and stiffness than high-expansion products; excessive deposit can reduce stretch comfort | Best for elastic garments and performance apparel |
| Soft-Hand Foaming Paste | Premium T-shirts, babywear, underwear, lightweight knits, and garments where comfort is important | Low to moderate expansion with emphasis on a smooth, flexible hand | Soft, lightweight, and absorbent fabrics that need a comfortable surface | Often about 140–165°C, according to the formulation and textile requirements | Soft, lightly raised, and low-gloss | Comfortable touch, lower perceived print weight, and good suitability for skin-contact garments | Limited maximum height and may require careful mesh, stencil, and squeegee selection to avoid a weak effect | Best for comfort-focused apparel and premium soft garments |
| Opaque Foaming Paste | Dark cotton, colored garments, workwear, uniforms, and graphics requiring strong color coverage | Moderate expansion while maintaining a relatively dense, covering print film | Dark or saturated fabrics where the garment color could reduce print brightness | Usually about 150–180°C, depending on the curing system | Raised, dense, and more substantial than transparent or low-opacity effects | Improved coverage, stronger color contrast, and better visibility on dark textiles | Can feel heavier and may reduce the softness of lightweight garments; migration testing may be needed on polyester | Best for high-contrast raised graphics on dark fabrics |
| Transparent or Semi-Transparent Foaming Paste | Tonal effects, overprints, fashion textures, vintage graphics, and designs intended to reveal the base fabric | Low to moderate expansion with a translucent visual effect | Light or medium-color fabrics with an attractive base texture or color | Typically about 140–170°C, subject to the technical specification | Subtle, textured, and sometimes slightly glossy | Creates layered visual depth, preserves the underlying fabric color, and supports decorative effects | Limited coverage on dark fabrics and more variation in appearance when the base fabric is uneven | Best for tonal designs and decorative surface texture |
| High-Density Foaming Paste | Embossed lettering, premium labels, geometric graphics, and structured decorative prints | Controlled high deposit with pronounced height after expansion and curing | Firm, stable fabrics that can support a thick print without excessive deformation | Usually about 150–180°C, depending on the product system | Strongly raised, sharply defined, and often firm | Excellent dimensional impact, crisp edges, and premium tactile definition | More demanding screen preparation, slower production handling, heavier hand feel, and reduced suitability for drapey fabrics | Best for premium embossed effects on stable textiles |
Note: Curing temperatures and expansion levels are typical working ranges, not universal specifications. Always verify the technical data sheet, fabric heat tolerance, wash durability, and dye-migration performance before production.
Foaming paste creates a raised surface by expanding under controlled heat.
The best paste in 2026 is not simply the one with maximum volume. It should provide stable expansion, clean detail, soft hand feel, and reliable wash resistance. Grand View Research estimates the global screen-printing inks market will grow at about 3.8% annually through 2030. That growth reflects continuing demand for specialty finishes, including tactile effects.
Start with a clean, fully cured fabric. Use a mesh count recommended by the paste supplier, then print an even deposit with moderate pressure. Too much squeegee pressure can flatten the layer. Too little pressure may leave pinholes.
A test square helps. Record mesh, stroke speed, ink deposit, and curing temperature. Heat the print gradually until the surface expands evenly, usually within the supplier’s stated curing range.
Smithers’ global printing outlook identifies specialty effects as an important value-added direction, but consistency still depends on process control rather than paste alone.
Inspect the first print from the side.
Raised edges should look rounded, not cracked. Wash testing matters. Use the same detergent and cycle your customers may use. I often find that a slightly lower expansion gives better durability, although it looks less dramatic. That trade-off is easy to overlook. Foam can also collapse when the substrate contains moisture or uneven fibers. Allow extra drying time, and check several prints across the garment, not only the first one.
The best foaming paste is not always the cheapest option. A reliable comparison starts with expansion, surface definition, curing stability, and print consistency. Grand View Research valued the global textile printing market at approximately USD 2.5 billion in 2023. Its forecast also suggests steady growth through 2030. That growth increases pressure to reduce reprints and production waste.
Test each paste on the actual fabric. Cotton, blends, and dark garments can react differently. Record the wet deposit, curing temperature, foam height, and wash appearance. A raised print may look impressive initially. It can still collapse after repeated laundering. ISO 6330 washing procedures provide a useful reference for evaluating dimensional and appearance changes. Do not judge quality from one sample.
Cost needs a wider calculation. Compare price per kilogram, coverage per screen, curing energy, and rejected garments. Smithers’ Future of Global Printing to 2028 report emphasizes productivity and waste reduction as major competitive factors. A cheaper paste may require thicker layers or slower curing. That difference can erase the original saving. Small details matter.
Use a controlled trial. Keep mesh count, squeegee pressure, stroke speed, and curing time consistent. Then score each result from one to five. I would give extra weight to adhesion and repeatability. This method is imperfect, because workshop conditions change. Humidity alone can disturb results. Still, measured evidence is stronger than a glossy sample or an attractive quotation.